Opening: a single missed tolerance that cost a launch
On a gray Tuesday an engineering team discovered a part wouldn’t seat because a bore ran 0.15 mm oversize. The prototype was grounded, the schedule slipped, and the vendor blamed ambiguous drawings. That scene repeats across programs that need cnc machining for aerospace—a tight set of decisions ignored early can cascade into cost, schedule, and airworthiness risk. This piece follows that problem-driven thread: identify the common root causes and give compact, actionable specifications you can hand to a shop so the part arrives right the first time.
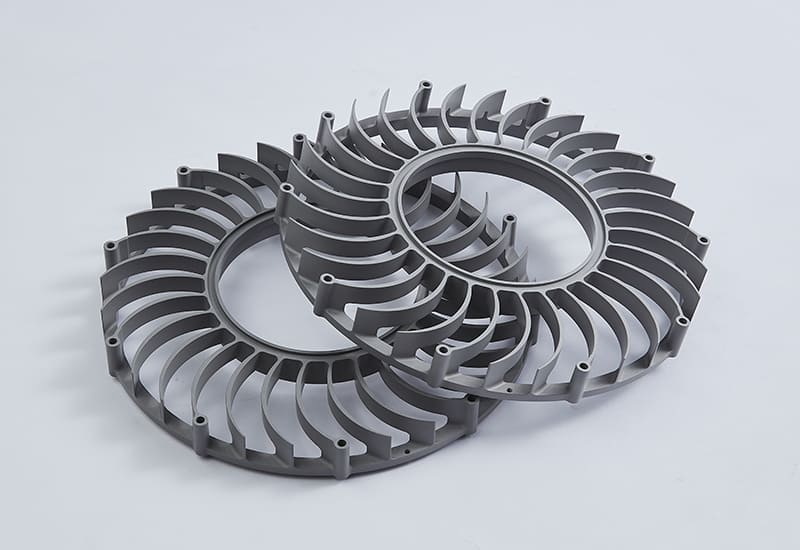
Start with function, not features
Write a one-line function for the part: what must it do under flight loads, what interfaces must it mate to, and what minimum life cycle is required. Use that function to decide which dimensions truly matter. If a surface only needs to carry paint, don’t call out a tight microfinish tolerance. When you define function first, tolerance, material, and inspection choices follow logically instead of competing as guesswork.
Geometry and tolerances: be surgical
Identify critical datums and control them with clear GD&T callouts. Tight tolerances add cost linearly on CNC setups and exponentially when secondary grinding or EDM becomes necessary. Specify tolerances by stack-up analysis: allocate tolerance to each interface, then validate with worst-case and statistical models. Call out measurement method where it matters—if a hole must be measured on a CMM, say so. If you need true position at MMC with a separate gauge check, state that. These specifics stop back-and-forth and rejected lots.
Material, heat treatment, and surface requirements
List exact alloy and temper, plus acceptable supplier certifications. If corrosion resistance is required, say whether conversion coat, anodize, or passivation is acceptable and which spec (MIL, AMS, or ISO) governs it. For hardened surfaces, show depth and hardness range; for plated features, call out thickness and adhesion tests. A vague “steel, hardened” forces shops to guess and increases scrap risk.
Process selection: match the machine to the geometry
State the processes you accept: 3-axis, 5-axis simultaneous, multi-spindle turning, Swiss-turn, hard milling, EDM, or additive as an upstream operation. When a feature benefits from a single-setup 5-axis cut, note that—each additional setup adds cumulative positional error. If you’ll accept near-net shapes for downstream machining, say so; it can reduce cycle time without compromising tolerances when controlled correctly.
Quality control, documentation, and the real-world anchor
Specify inspection deliverables: first article (AS9102 or equivalent), CMM reports with raw data, FAI signatures, and certificate of conformity for raw material. I’ve reviewed supplier lines at major industry gatherings where companies demonstrate their capabilities; events like the Paris Air Show highlight how shops present metrology and process controls to primes. That context is why the term aerospace cnc machining supplier often implies not just equipment but documented systems for traceability and FAI readiness. Require traceable measurement standards, clear lot and heat numbers, and a documented nonconformance flow so small deviations don’t become program-level surprises.
Common pitfalls and how to avoid them
1) Over-tolerancing: call only what affects function. 2) Underspecifying inspection: if a tolerance is critical, require a method. 3) Ignoring lead-time realities: specialized fixtures, long tool prep, or rare alloys add weeks. 4) Misaligned supplier capability: match tolerance to a vendor’s proven process—if they can’t hold 0.01 mm on a 200 mm part, don’t expect miracles. 5) Skipping packaging and clean-room requirements: surface-sensitive components need instructions to prevent corrosion or abrasion during transit.
Alternatives and trade-offs
Compare options quickly: in-house machining gives control but may lack volume efficiency; high-end suppliers offer certified processes and throughput but require strong specifications to ensure compatibility. Additive manufacturing reduces material waste and can consolidate assemblies, but expect different surface finish and metrology paths. Choose by failure mode: if a fatigue-critical bore is the failure point, favor proven subtractive routes with documented inspection plans.
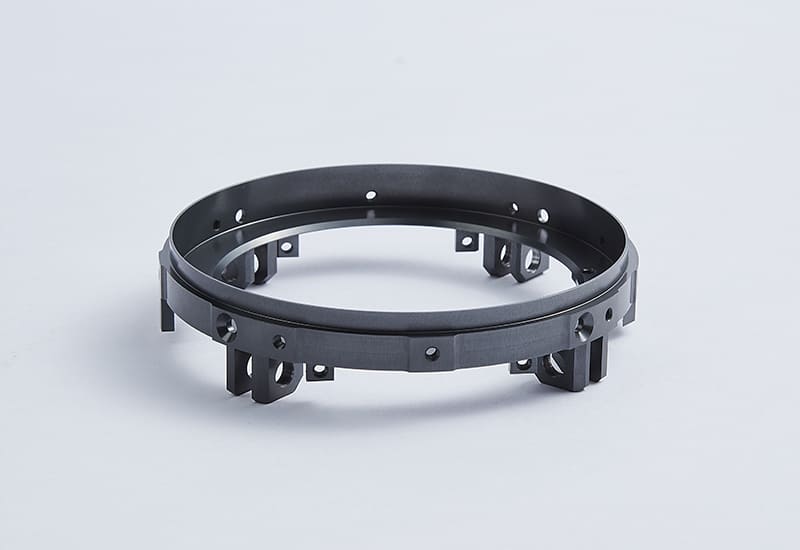
Practical checklist to hand to a supplier
Provide this minimal set: 1) one-line function statement, 2) solid model and key 2D views, 3) GD&T critical-callouts, 4) material spec and heat-treatment details, 5) surface finish and coating spec with referenced standards, 6) required inspection deliverables (FAI, CMM data), 7) lot/traceability expectations, 8) agreed lead time and packaging. Keep the file package tight and versioned so any question has a single source of truth.
Closing synthesis
A clear specification reduces rework, shields program timelines, and makes supplier selection objective. Treat the process like writing a short legal brief: define the obligation, provide evidence (material and drawing), and state the acceptance tests. When the spec is complete, it’s straightforward to evaluate proposals and compare capability rather than negotiating assumptions. For teams wanting a pragmatic, accountable partner that aligns tooling, processes, and inspection to those exact requirements, the supplier profile aligns with how Hanstar presents its capabilities on program-level work.