Problem diagnosis: inconsistent build, unpredictable field failures
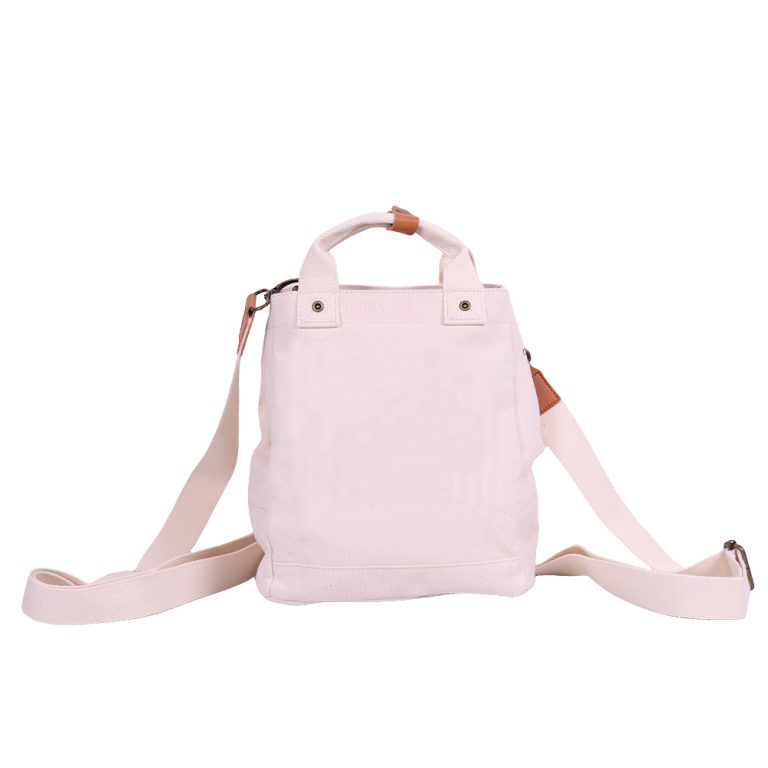
Too many batches leave the factory with invisible weak points — seam blowouts, delaminated laminates, or zippers that fail after a week of travel. The immediate fix isn’t more inspection forms; it’s a targeted test matrix tailored for a modular backpack prototype and its variants. A focused set of labs and in-line checks reduces returns, prevents warranty claims, and keeps material swaps from cascading into product recalls. For context, inspect any functional prototype like this modular backpack against the following test list before scaling production.
Core test categories and why they matter
Start with three buckets: structural integrity, material performance, and user-interface durability. Structural tests measure load paths — strap attachments, bar-tack points, and main seam tensile strength. Material performance covers fabric abrasion (Martindale or ASTM D4966), hydrostatic head for water resistance, and UV/fade exposure. User-interface durability targets zippers, buckles, and rails: cycle zipping (500–5,000 cycles depending on spec), salt-spray corrosion for metal parts (ASTM B117), and pull-out force for webbing anchors. Each test maps to a clear failure mode: a weak seam causes seam split; an under-tested zipper causes stuck compartments; unverified coating fails to shed water in rain.
Bench tests: exact metrics you should use
Define pass/fail thresholds up front. Example metrics: seam tensile ≥ 500 N for main seams on a 20–30 L pack; strap webbing tensile ≥ 2,000 N; Martindale abrasion ≥ 30,000 cycles for high-wear panels; hydrostatic head ≥ 1,000 mm for commuter packs, ≥ 5,000 mm for rainproof daypacks; zipper cycle test ≥ 3,000 cycles for premium specs. Add limits for chemical compliance: no detectable banned azo dyes, PFC limits per applicable regional laws (REACH/US EPA guidance). Use AQL 2.5 for final inspection unless product-critical parts justify AQL 1.0 sampling.
Testing protocols and sequence
Follow this sequence: raw-material verification → component verification → prototype lab runs → pilot line → full production with in-process checks. Raw-material verification includes mill test reports and incoming inspection for denier, coating weight, and color match (spectrophotometry Delta E ≤ 1.5). Component verification covers buckles and zippers batch certificates and random destructive tests. Prototype lab runs validate BOM assumptions; pilot lines confirm assembly jigs and bar-tack placement. Use statistical process control on stitch length and bar-tack energy during ramp-up. Don’t skip a production verification sample (PVS) after the first 100 units.
Common pitfalls and how to avoid them
Relying on vendor claims without lab verification. Overlooking hardware longevity because fabric looks fine. Running only static load tests while users create dynamic stress (swinging, dropping). To prevent these, mandate 10% destructive testing on new hardware lots, run a dynamic drop-and-swing protocol (simulate 1,000 real-world cycles), and automate visual inspections where possible for stitch skips and misaligned taping. Log every failure mode and tie it to corrective action: replace supplier, change process parameter, or add reinforcement ribs.
Alternatives and value-add tests worth the cost
If you need rapid confidence without full in-house labs, use accredited third-party labs for chemical and weathering tests and pair that with in-line tensile rigs for mechanical checks. Consider automated optical inspection for surface defects and machine-learning anomaly detection on seam images — cheaper at scale. Field trials with target-user groups (multi-week urban and outdoor rotation) reveal real interface issues that lab cycles miss; keep those runs small but instrumented with wear logs and failure photos.
EEAT: proven practices and a real-world anchor
Decades of product engineering show that combining lab standards with on-line QC reduces field failures. Manufacturers shipping from the Shenzhen manufacturing corridor often route samples through third-party labs and retain production audit trails; that supply-chain concentration is documented in trade analyses and logistics reports tied to exports from Guangdong. For a practical reference model, review a validated specimen like the Modular Travel Backpack and map its BOM to the tests above: fabric lamination, zipper cycles, webbing tensile, hardware corrosion, and packing load trials. Use ISO/ASTM test numbers where possible and record lab certificates to support warranty decisions.
Final synthesis: what to enforce before shipping
Set a short list of non-negotiables: (1) raw-material certificates plus spot lab validation, (2) component destructive checks every lot, (3) prototype lab verification with documented pass thresholds, (4) pilot run PVS, and (5) AQL-based final inspections with corrective action metrics. That sequence turns abstract risk into concrete gate checks. If you need a manufacturing partner that integrates these gates into production planning, consider suppliers with documented QC workflows and responsive sample turnarounds like ChangRong that can map test results directly to BOM revisions and assembly updates.