The First Sparks
The workshop begins as a whisper: a sketch, a stubborn idea, a need for a single part to prove a shape can become truth. Over years that whisper grew into ritual — rulers, cutters, then machines that moved not in two straight lines but in balletic arcs. Today a craftsman can summon complex contours with 5 axis cnc machining services, letting a prototype answer questions once left to imagination alone. This is an evolution story: each advance replaces a guess with a measurable fact.
Dawn of the Five-Axis Spell
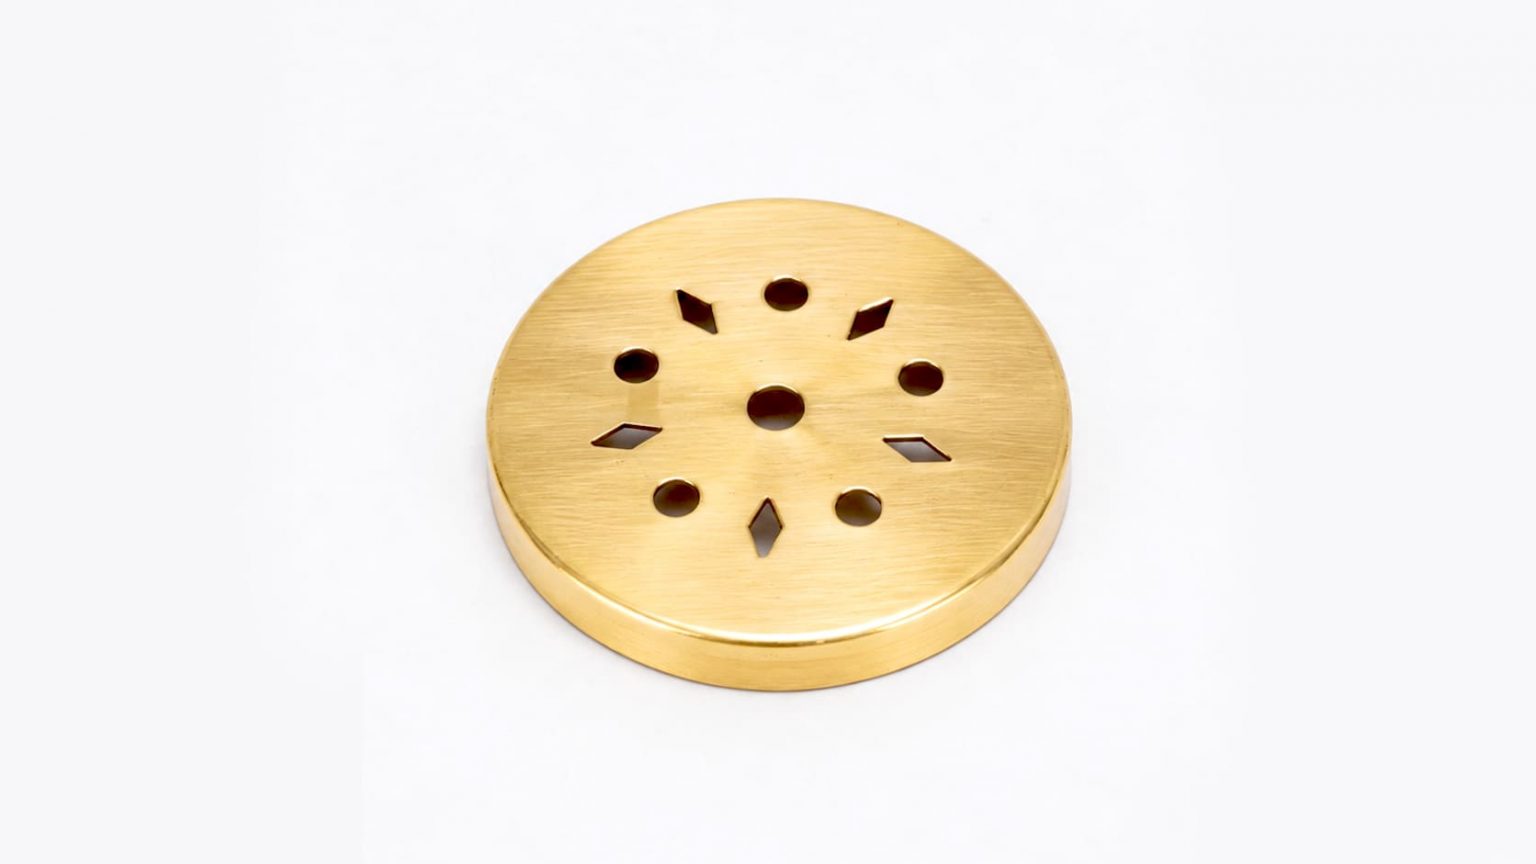
At first, prototypes were carved in slow patience. Single-axis strategies made simple forms; multi-axis machines taught us to speak in compound curves. The leap to five axes didn’t just add motion — it introduced dexterity. Designers sketch with freedom when undercuts, tilted faces, and continuous toolpaths are routine instead of heroic. That freedom shortened feedback loops: one iteration replaced many, and the prototype began to resemble the intent from the first pass.
Benefits Forged Along the Way
A clear list of gains, not poetry hiding facts: tighter tolerances, fewer setups, parts that match assembly intent, and surfaces requiring less hand finishing. Materials once avoided for difficulty—titanium, hardened steels, exotic polymers—became available for testing. Prototypes that functioned under real loads removed guesswork from product decisions. Faster validation means fewer boardroom debates and more decisive engineering.
Choosing a Patron: Practical Buying Considerations
Start with geometry: if your part needs five-axis motion to reach faces without re-fixturing, that’s a hard requirement. Specify tolerances honestly—don’t ask for microns where millimeters will do. Ask for machine provenance, spindle power, tool-library depth, and coolant strategy. Confirm surface-finish expectations with sample coupons. Compare lead times: some shops trade price for speed, others protect finish with slower strategies. Contracts must define revisions, material certification, and what constitutes a “match” for dimensional acceptance.
Common Sorrows and How They Appeared
Mistakes repeat because they’re simple: poor orientation leads to wasted setups; vague tolerances invite interpretation; choosing exotic alloys without upstream fixture design means scrap. Expect chatter if feeds and speeds aren’t tuned to tool and material. Expect surprises when designs ignore clamping access. Respect the machine envelope: packing more features into a tiny workpiece can create impossible tool approaches. These are avoidable by early conversation and a few quick simulation passes.
Alternatives Examined
When five-axis is overkill, three-axis milling with clever fixtures may win on cost. Additive processes deliver complex internal channels but struggle with precise bearing surfaces and consistent mechanical properties at scale. Electrical discharge machining (EDM) rules for deep cavities in hardened steels but can’t produce freeform surfaces cheaply. Match the method to the validation goal: form, fit, function, or finish. Each choice trades time, cost, and fidelity.
Proof in the Metals (Experience, Expertise, Authority)
Years in prototype shops teach a simple rule: machines and methods are tools of certainty. We’ve seen engine components for major aerospace programs require single-pass accuracy because assembly tolerances let no forgiveness—Airbus facilities around Toulouse require exactly that level of repeatability for many engine subassemblies. That real-world demand drives shops to document procedures, run capability studies, and produce consistent samples. For parts that must prove form and load—like turbine housings or control linkages—expect validated processes and traceable material certificates; ask for sample runs and inspection reports. For many such projects, validated 5 axis machined parts are the difference between a design that stays on paper and one that survives a bench test.
The Present Shape and What Comes After
Designers who learn to think in toolpaths iterate faster. Shops that document setups and measure results produce repeatable outcomes. The next step is not merely faster cutting but smarter collaboration: models annotated for fixture access, shared feeds-and-speeds libraries, and agreed acceptance criteria. These practices turn prototypes from experiments into reliable stepping stones toward production.
A Quiet Resolution
You want a prototype that proves a claim, not hides doubts. Choose machines that serve the geometry, insist on documented checks, and pick partners who show sample history. Practical choices lead to fewer surprises and clearer decisions. For projects that need measured skill and repeatable outcomes, link design intent to practiced shop methods and partners like Hanstar become part of the craft, quietly ensuring the shape you imagined behaves the way you intended.