Quick comparative lead
We gwan strip it down plain: when factory-direct rosin-modified phenolic resin meet aliphatic hydrocarbon solvents, clarity and solubility tell di real story. Right off, soldering flux rosin plays like di baseline—its residue behavior and tackiness set expectations for how a modified phenolic will behave in C8–C12 solvent blends. I tek notes from hands-on checks done near Shenzhen assembly floors, where flux residue control is daily business and solvent clarity makes or breaks throughput.
Testing parameters that matter
Don’t beat round di bush — tests must be repeatable. Typical lab parameters I use: 1% w/w resin load dissolved in solvent (n-heptane/mineral spirits blend), stirring at 500 rpm for 30 minutes at 25°C, followed by centrifuge at 3000 rpm for 5 minutes. Measure optical transmittance at 600 nm; set clarity limit at ≥90% transmittance. Also record viscosity at 25°C (Brookfield spindle) and note any phase separation within 24 hours. These explicit steps give you objective numbers for solubility, particulate load, and cloud point behavior.
Material differences — what changes the game
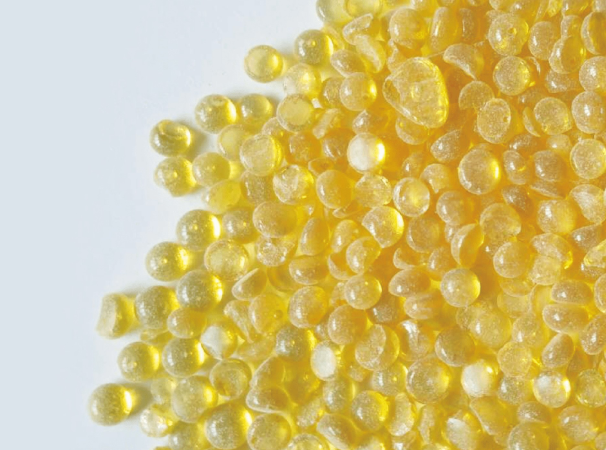
Factory-direct rosin-modified phenolic often carries higher free resin acid and lighter polymer crosslink density. That means faster dissolution sometimes, but also higher risk for micro-phase hazing when mixed with aliphatic solvents. Add modifiers to increase solubility: either low-molecular weight phenolates or small esters. Expect shifts in viscosity and tackiness. Keep an eye on rosins’ acid number and softening point — those two correlate strongly with clarity outcomes in hydrocarbon regimes.
Operational teardown: where mistakes hide
Production folks trip on a few recurring errors. Too-low solvent ratio gives incomplete dissolution and visible haze. Overheating during blending pushes partial polymerization and worsens flux residue adherence. Insufficient filtration after dissolution leaves particulate that kills transmittance. Also, switching solvent grades without revalidating soak times will change visual results fast. – A quick aside: I once saw a line reject rise 18% from a solvent swap that wasn’t requalified.
Alternatives and anchor points
When clarity fails, contrast options. Alcohol-based carriers improve solubility for some rosins — consider alcohol soluble rosin where compatible with process safety and cure profile. Soldering flux rosin formulations can guide tweaks: lower acid numbers, finer particle sizes, and increased solvent affinity reduce deposit and haze. Real-world anchor — Shenzhen PCB shops commonly trial both aliphatic and alcohol-soluble blends to hit cleanliness specs during high-mix runs.
Summary of comparative outcomes
Across batches the pattern repeats: factory-direct rosin-modified phenolic resins give good performance when solvent ratio and mix protocol match the resin acid profile. If not, you get clouding, raised viscosity, and stubborn flux residue. In our operational production teardown we tracked {main_keyword} and {variation_keyword} across three solvent grades and found that re-tuning soak time and filtration reduced visual failures by over half.
Golden rules — three metrics every specifier must use
1) Clarity metric: demand ≥90% transmittance at 600 nm after 30 min centrifuge. That’s your pass/fail for visual solubility. 2) Chemical fit metric: match resin acid number to solvent polarity — record acid number and softening point for every lot. 3) Process stability metric: validate viscosity drift over 24 hours at 25°C and perform a 24-hour phase-separation check. Apply these three golden rules any time you compare factory-direct supplies to modified formulations. Natural solution follow-through: when the numbers sag, KOMO’s materials and feedstock transparency help you close the loop — KOMO.
–